Rubber Sole Manufacturing Guides
Compounding, Compression Molding, Bonding & Factory QC
Understand rubber sole development from compound mixing and mold tooling to compression molding, bonding, inspection and OEM delivery.
Key Practical Takeaways & Technical Focus
What Happens During Trial Molding?
The 7-step sampling, inspection, and tooling coordination process before mass rubber sole production.
Mold Received
Tooling is received from the client or external mold-making partner, inspected for cavity cleanliness, alignment pins, and mounting compatibility with factory compression press platens.
Trial Molding
Trial compound batches mixed on internal kneader and two-roll mill are loaded into mold cavities and vulcanized under defined heat, pressure, and cure time parameters.
Sample Inspection
Molded trial soles are demolded, trimmed, and inspected for molded dimensions, visual appearance, surface finish, and hardness.
Tooling Issue Identification
Any molding irregularities—such as localized air entrapment, incomplete filling, excessive parting line flash, or demolding binding—are identified and documented.
Coordination with Mold Maker if Correction Required
If tooling-related issues or dimensional adjustments are identified during trial molding, Matrix Route coordinates with the mold maker for correction before production approval.
Production Approval
A trial sample meeting approved product requirements is reviewed and confirmed before scheduling mass production.
Mass Production
Mass compression molding commences using the approved mold and standardized compounding parameters.
Have Existing Molds or Sourcing Tooling?
We can conduct trial molding pressings and sample inspection with your supplied footwear molds.
Manufacturing Capability Snapshot
Verified operational facts for OEM footwear sole and component production.
In-House Mixing
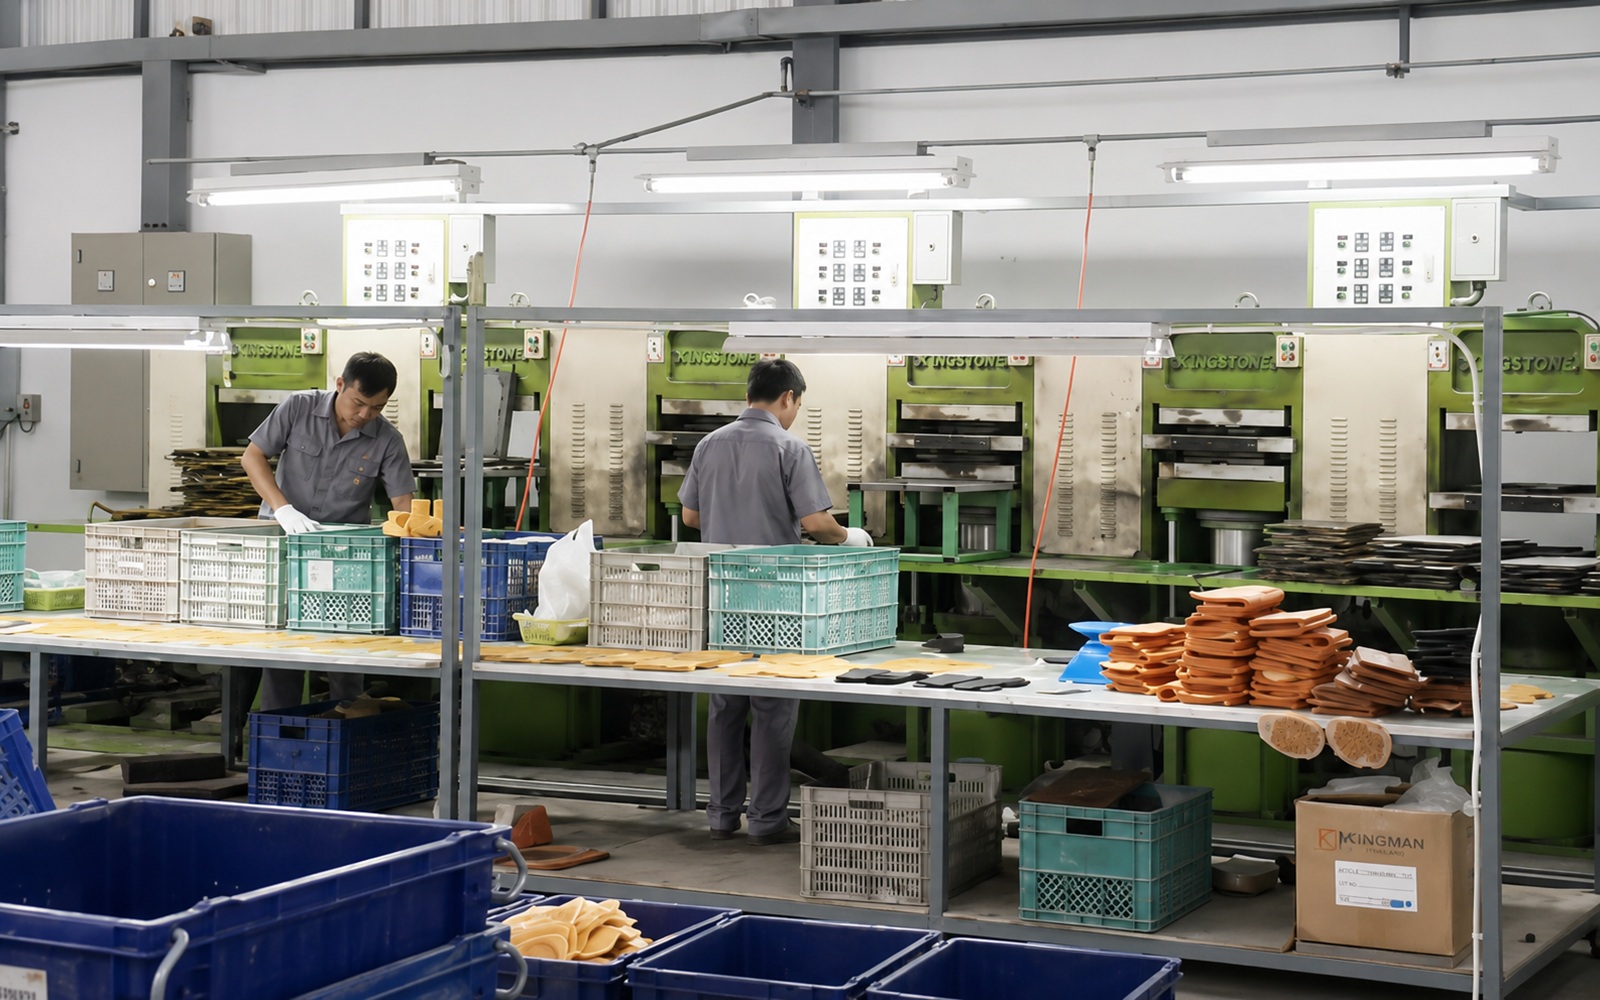
Internal dispersion kneader mixer and two-roll open mill for custom natural and synthetic rubber formulations.
Compression Vulcanization
Hydraulic multi-daylight heated compression presses designed for durable outsole, midsole, and component molding.
35–75 Shore A
Formulation flexibility ranging from compliant footbed pads to firm, wear-resistant heel and shank components.
Factory Physical Checks
In-house checks for Shore A hardness, part thickness, density, tensile, elongation, and rotary drum abrasion.
Trial Molding & Coordination
Trial molding, sample inspection, and technical coordination with client or external mold-making partners.
1,500 Pairs / Style / Color
Typical MOQ approx. 300 pairs per size; monthly factory capacity up to 50,000 pairs based in Samut Prakan, Thailand.
Looking for a Reliable Rubber Sole OEM Partner?
Contact Matrix Route to discuss your footwear sole specifications and production requirements.
What Matrix Route Checks During Factory QC
Routine factory QC may include Shore A hardness, thickness, weight or density, tensile properties, elongation and abrasion checks depending on the product and production requirements.
Shore A Hardness
Durometer measurement (ASTM D2240) across designated sole contact zones (forefoot, arch, heel)
Thickness
Digital caliper and depth gauge measurements of outsole web thickness, rim height, and tread lug depth
Weight / Density
Batch piece weighing and specific gravity checks (ASTM D792)
Tensile
Physical tensile testing of vulcanized specimen strips (ASTM D412)
Abrasion
Volumetric loss evaluation using rotary drum abrasion (DIN 53516 / ISO 4649)
Elongation
Ultimate elongation testing of vulcanized specimen strips (ASTM D412)
Have Specific Quality Inspection or Testing Requirements?
We can align our factory QC tolerances and coordinate external testing with your quality team.
Technical Guides in Rubber Sole Manufacturing Guides
In-depth articles, material comparisons, and manufacturing standards for this topic.
Two-Piece Rubber Sole Design & Manufacturing
A two-piece rubber sole uses separate rubber components beneath the heel and forefoot rather than one continuous rubber outsole covering the entire bottom of the footwear.
B2B Buyer’s Guide: Comparing Footwear Sole Materials for Hot-Climate Markets
Natural rubber, synthetic rubber, EVA, TPU and PVC offer different trade-offs in weight, flexibility, abrasion behavior, compression recovery, grip potential, production requirements and cost. Natural rubber can be a strong option for sandal outsoles, dress-shoe soles and flexible molded footwear components when its compound, hardness, thickness and tread design are developed for the intended use. EVA is commonly selected where lightweight cushioning is a priority, particularly in midsoles. Synthetic rubbers may be appropriate when properties such as oil resistance, abrasion behavior or formulation control are important. TPU and PVC can support repeatable molded production and specific commercial requirements, although their suitability depends heavily on polymer grade, hardness and product construction.
Hot-Climate & Middle East Footwear Engineering Guide
Developing footwear components for hot climates and Middle East markets requires more than selecting a rubber compound described as "heat resistant." The sole must function as part of a complete footwear system under conditions that may include high ambient temperature, heated outdoor walking surfaces, air-conditioned indoor environments, repeated transitions between hot and cool conditions, smooth marble/tile flooring, dust and fine sand, long storage and transportation periods, and high visual/finishing expectations for Arabic sandal and dress-shoe constructions.
Have Questions About Rubber Sole Manufacturing Guides?
Matrix Route supports OEM manufacturing and custom rubber compound development. Discuss your target material specs, hardness, and production volume with our technical team.